
Laser cutting galvanized steel on a fiber laser works well, and shops do it every day. The zinc coating is the complication. It boils at a far lower temperature than steel melts, so it vaporizes ahead of the cut, produces a heavy white fume that has to be captured, tends to leave more dross and spatter than bare steel, and burns back from the edge so the cut face and a thin band beside it lose their corrosion protection. Manage those four things and galvanized cuts cleanly; ignore them and you get rough edges, a coated nozzle, and an operator breathing zinc oxide.
This guide covers how galvanized steel behaves under the beam, which assist gas to use and why, the parameter changes that keep the edge clean, the safety side that cannot be skipped, and what to tell customers about the edge afterward. It fits alongside our material guides on cutting stainless steel and cutting aluminum with a fiber laser.
Table of Contents
- Laser Cutting Galvanized Steel: The Short Answer
- What Galvanized Steel Actually Is
- What the Zinc Does Under the Beam
- Hot-Dip vs Electrogalvanized vs Galvanneal
- Which Assist Gas to Use
- Parameter Adjustments That Keep the Edge Clean
- Fume, Safety, and Extraction
- What Happens to Corrosion Protection at the Edge
- 7 Common Problems and Their Fixes
- Frequently Asked Questions
Laser Cutting Galvanized Steel: The Short Answer
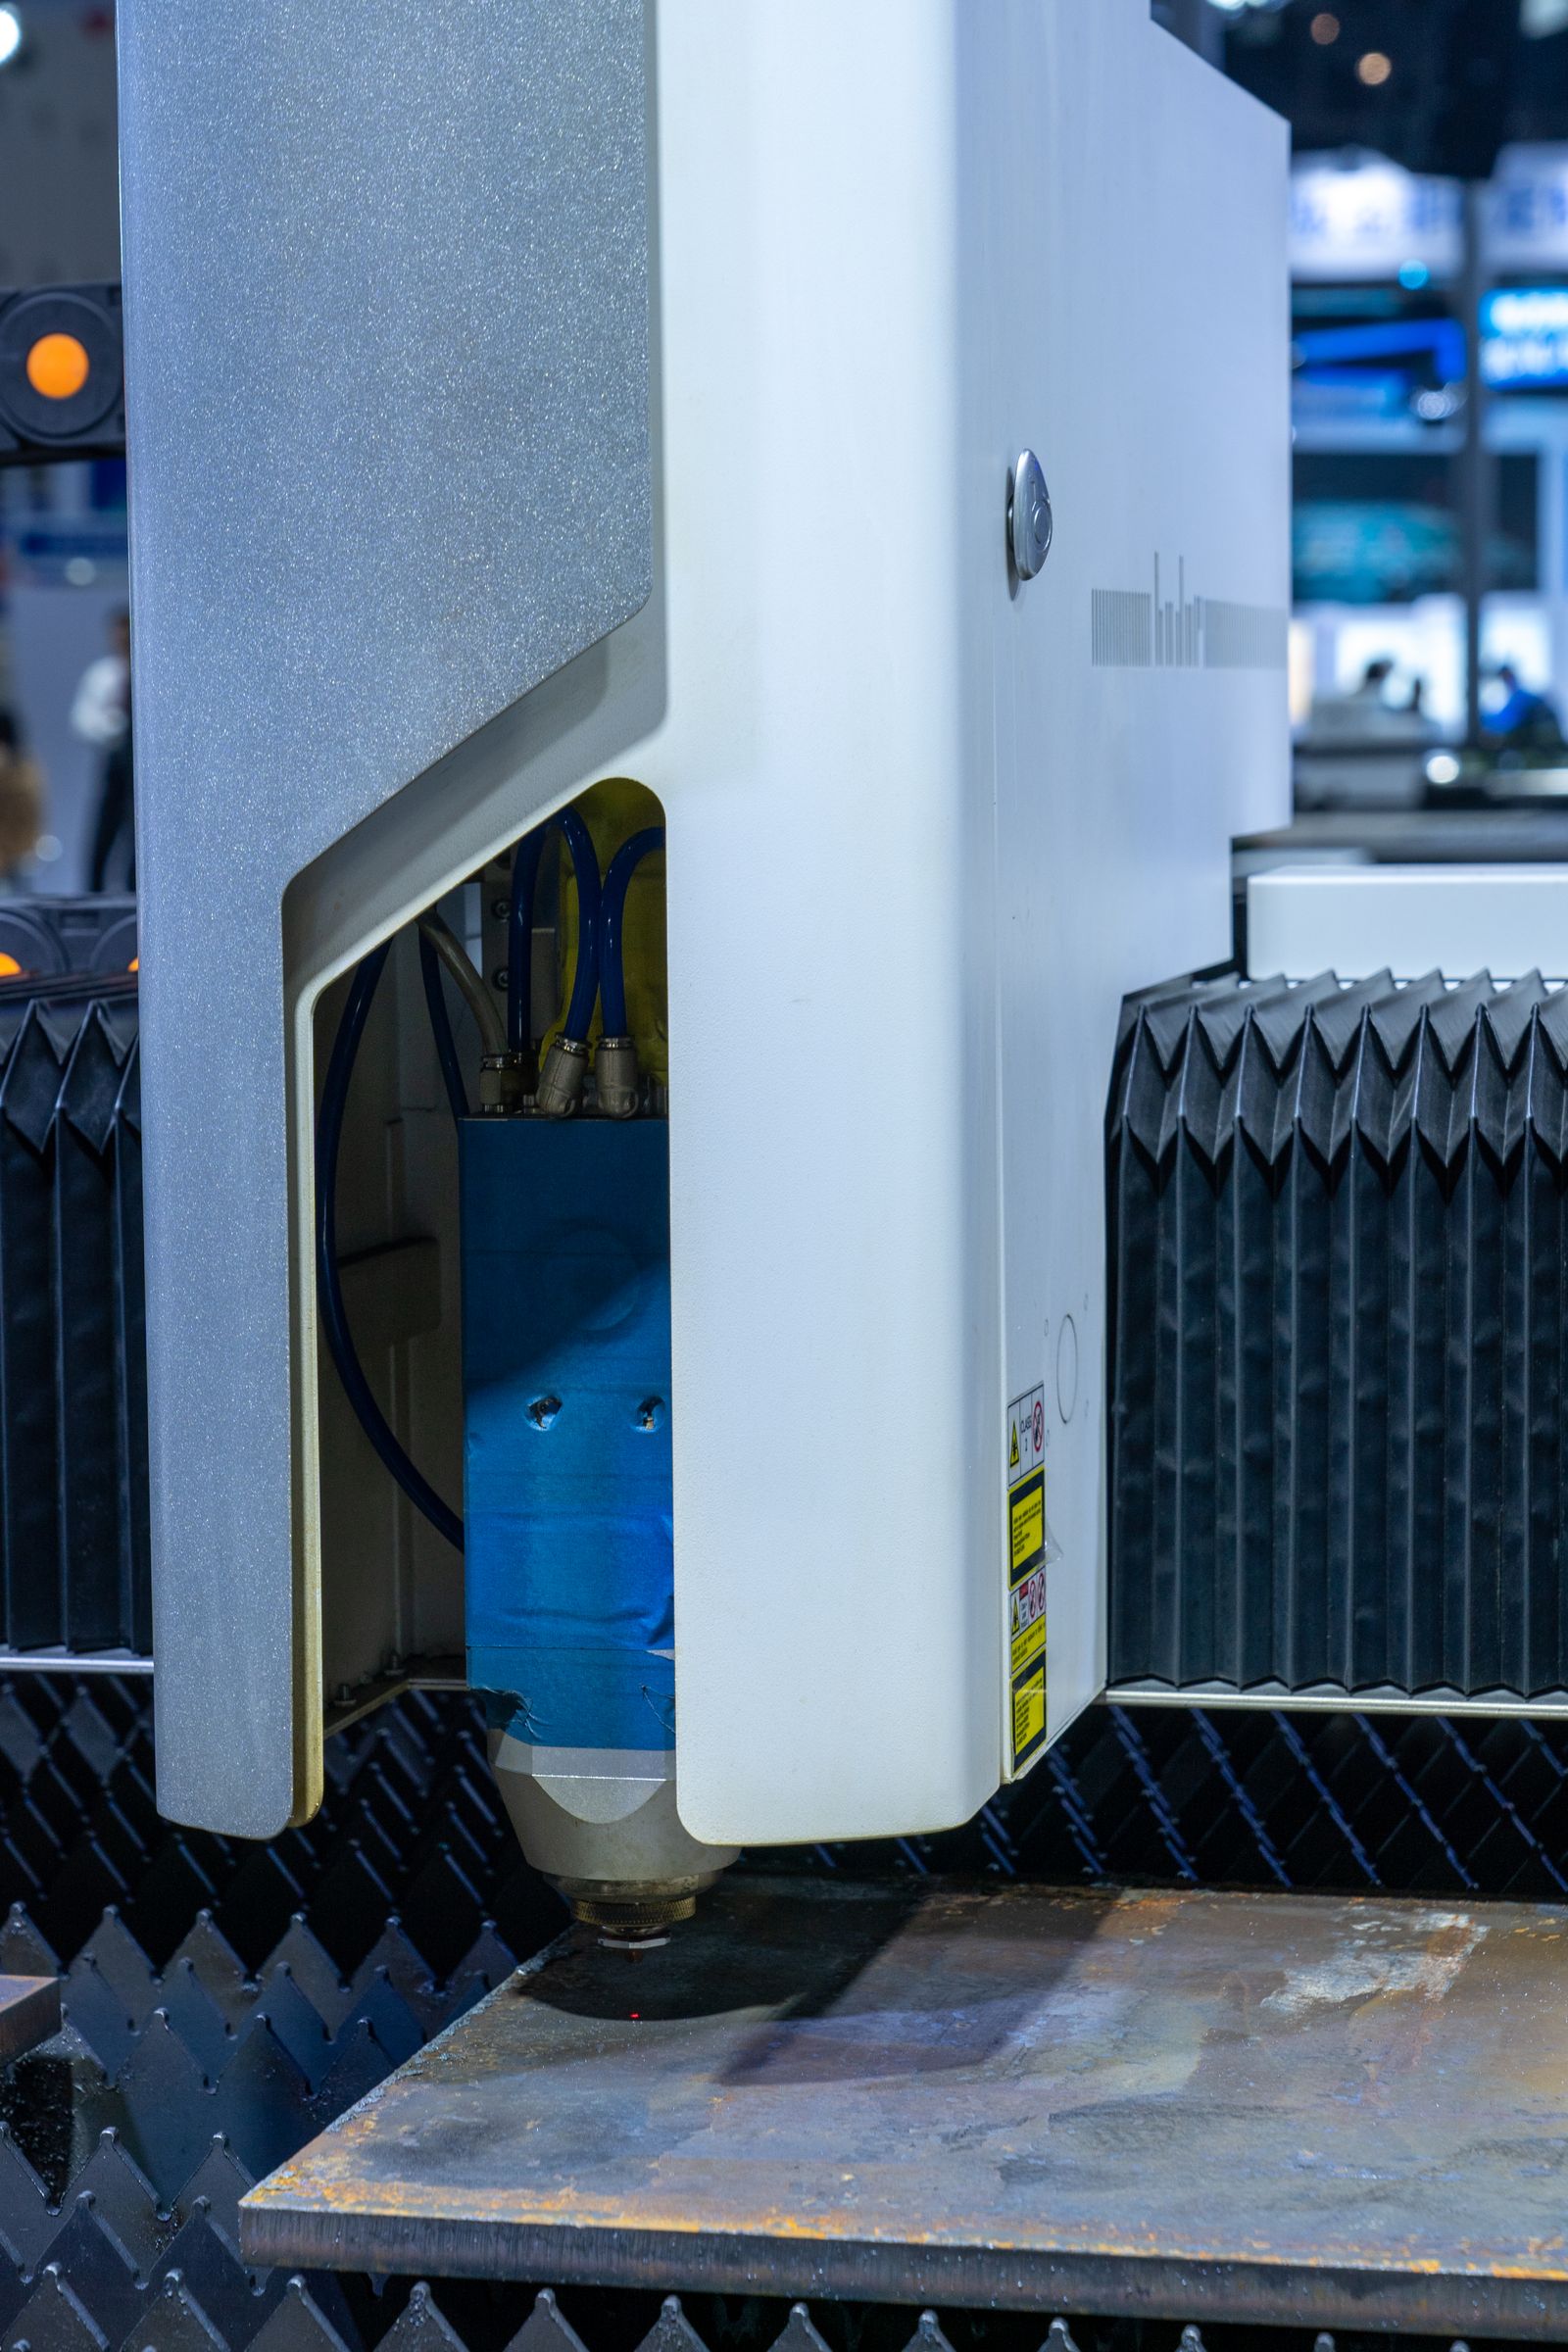
Yes, a fiber laser cuts galvanized steel, at speeds close to bare mild steel of the same thickness. The differences are in the details. Nitrogen or compressed air gives the cleanest edge, because the zinc does not react with an inert gas the way it reacts with oxygen. Feed rate usually comes down slightly and gas pressure goes up slightly compared to bare steel to blow the extra melt clear. Fume extraction has to be working properly, because zinc oxide fume is a genuine health hazard. And the finished edge should be treated as bare steel for corrosion purposes, since the coating is gone where the beam passed.
What Galvanized Steel Actually Is
Galvanized steel is ordinary carbon steel with a zinc coating bonded to the surface to stop rust. Zinc protects the steel two ways: it forms a physical barrier, and because it is more reactive than iron, it corrodes preferentially and sacrifices itself to protect any small area of exposed steel nearby. That second property is why a scratch in galvanized steel does not rust the way a scratch in painted steel does, and it matters later when we get to the cut edge.
The coating is thin, measured in fractions of a mil for light electrogalvanized sheet up to a few mils for heavy hot-dip material, but it is enough to change how the first moments of every cut go. The steel underneath behaves exactly like the mild steel you already cut. Everything different about galvanized is the zinc.
What the Zinc Does Under the Beam
Zinc melts at about 787 degrees Fahrenheit and boils at about 1,665. Steel melts around 2,700. So when the beam hits a galvanized sheet, the zinc on the top surface has vaporized before the steel underneath has even started to melt, and the zinc on the bottom surface flashes off as the melt breaks through. That vapor pressure is part of what pushes spatter around during the pierce, and it is why galvanized tends to leave more adherent dross on the bottom edge than bare steel does at the same settings.
The vaporized zinc condenses instantly into zinc oxide, the fine white smoke you see and the white dust that collects on slats and inside the enclosure. Some of it lands back on the sheet near the kerf as a chalky deposit, which is cosmetic. Some of it lands on the nozzle, which is not, because a coated nozzle changes gas flow and height sensing. And the heat of the cut burns the zinc back from the edge a short distance on both faces, leaving a narrow band of bare steel beside the kerf.
Hot-Dip vs Electrogalvanized vs Galvanneal
Not all galvanized sheet cuts the same, because the coatings differ.
- Hot-dip galvanized (G60, G90, and similar). The sheet is dipped in molten zinc, leaving a relatively thick, sometimes spangled coating. More zinc means more fume, more spatter, and more dross. Heavier coatings such as G90 are the hardest to cut cleanly and want the most gas pressure.
- Electrogalvanized. Zinc is plated on electrically, producing a thin, uniform, matte coating. It cuts closest to bare steel and is the easiest galvanized product to get a clean edge on.
- Galvanneal. Hot-dip galvanized that has been heat-treated so the zinc alloys with the iron at the surface. The coating is a zinc-iron alloy, dull gray, and it cuts more like electrogalvanized than like heavy hot-dip, with somewhat less spatter.
If a customer’s drawing just says galvanized, ask which. The parameter set that gives a clean edge on 16 gauge electrogalvanized will leave dross on 16 gauge G90.
Which Assist Gas to Use
Nitrogen is the usual choice for galvanized sheet. Because nitrogen is inert, the zinc vapor and the steel melt are simply blown out of the kerf rather than burned, which produces a brighter, cleaner edge with less oxide and less adherent dross. Nitrogen also leaves an edge that takes paint and powder coat without cleanup, which matters because galvanized parts are often finished after cutting.
Compressed air works well on thinner galvanized sheet and costs far less than nitrogen. Air is roughly four-fifths nitrogen, so the edge is nearly as clean, with a light oxide tint that is acceptable for most work that will be painted or hidden. Many shops run air on galvanized up to about 10 gauge and switch to nitrogen only when the edge finish is specified.
Oxygen cutting is possible but usually not the best choice. The exothermic reaction that makes oxygen so effective on thick mild steel also reacts with the zinc, which increases dross, roughens the edge, and burns the coating back further. Oxygen makes sense mainly on thick hot-dip plate where the speed advantage outweighs the edge quality penalty. Our guide to laser cutting assist gas covers the tradeoffs in more depth.
Parameter Adjustments That Keep the Edge Clean
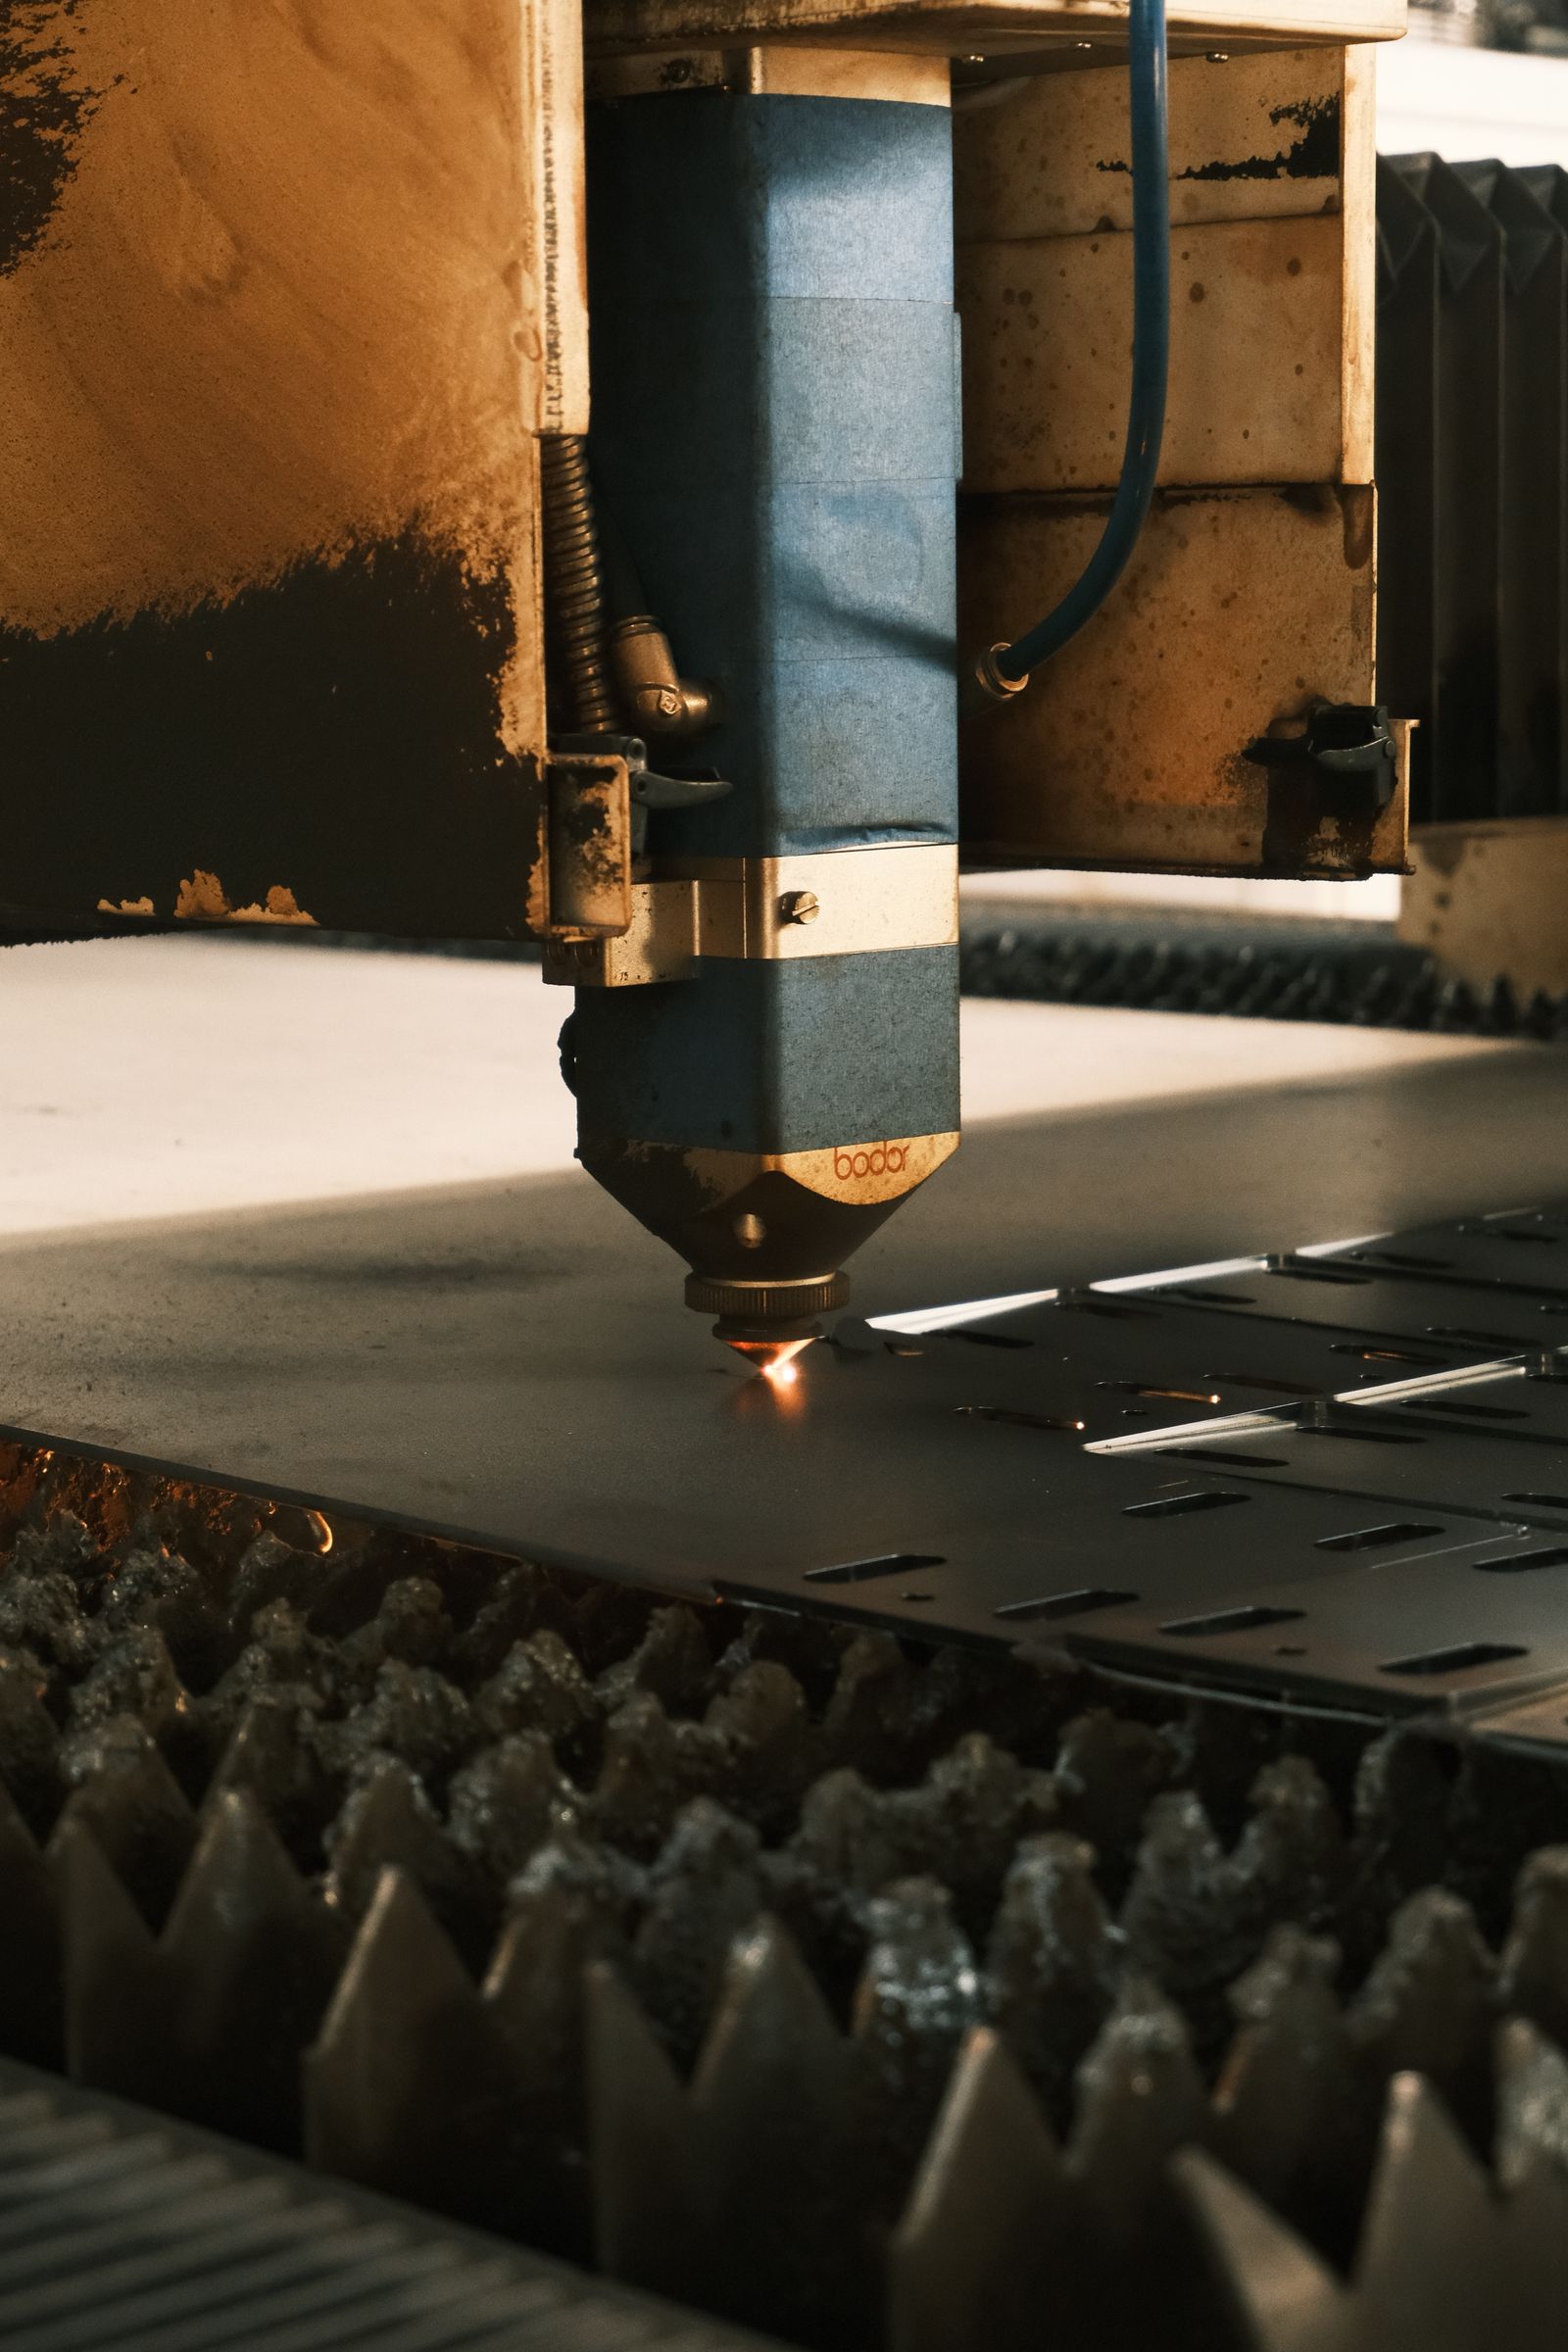
Start from your bare mild steel parameters for the same gauge and the same gas, then make these adjustments.
- Reduce feed rate slightly. The zinc adds melt volume and vapor turbulence in the kerf. Backing off speed by a modest amount gives the gas time to clear it. Going too slow overheats the edge and widens the burn-back band, so adjust in small steps.
- Increase gas pressure a little. The extra melt and vapor need more force to eject cleanly, especially on heavy hot-dip coatings. This is the single most effective change for dross.
- Keep focus at or slightly below the surface. A focus set deep in the sheet, as for thick nitrogen cutting, is not needed on thin galvanized and tends to increase bottom dross.
- Use a gentler pierce. The zinc flashes off violently during the pierce. A ramped or staged pierce with lower initial gas pressure throws less spatter at the nozzle and protective window.
- Check the nozzle more often. Zinc oxide builds up on the nozzle face faster than bare steel spatter does. A coated nozzle throws off height sensing and gas flow, and the first sign is usually a dross line that appears mid-sheet.
The starting values in our post on fiber laser cutting parameters by material and thickness apply to the base steel, and the adjustments above sit on top of them.
Fume, Safety, and Extraction
This is the part that cannot be treated as optional. Inhaling zinc oxide fume causes metal fume fever, a flu-like illness with chills, fever, and nausea that shows up hours after exposure. It is the same hazard welders face on galvanized material, and a laser cutting a full sheet produces it continuously. Modern fiber lasers are fully enclosed, which contains the fume, but the enclosure only works if the dust collector is pulling enough air through it and the filters are not loaded.
Practical rules: confirm the extraction system is running and pulling at its rated airflow before the first galvanized sheet of the day, keep the enclosure doors closed during the cut, let the enclosure clear before opening it, and replace or clean filters on the schedule that the dust collector manufacturer specifies, which will be shorter than for bare steel. Zinc oxide dust accumulates on slats and in the machine bed as well, so cleanout should be done with respiratory protection and without dry sweeping. The OSHA guidance on zinc is the reference for exposure limits, and our post on fiber laser operator training covers the general safety framework.
What Happens to Corrosion Protection at the Edge
Where the beam passes, the zinc is gone. The cut face is bare steel, and a narrow band on the top and bottom surfaces beside the kerf has lost some or all of its coating to heat. On heavy hot-dip material that burn-back band is visible as a darker line along every edge.
For many applications this does not matter. Zinc’s sacrificial action protects small areas of exposed steel next to intact coating, so a thin cut edge on a part that lives indoors will typically stay rust-free for a long time. For parts that live outside, in wet conditions, or in corrosive environments, the edge is a weak point, and the customer should know that. Options are to prime and paint the edges, apply a zinc-rich touch-up coating, or specify that the part be galvanized after fabrication rather than cut from pre-galvanized sheet. Which one is right is the customer’s call, but it is worth raising before the parts ship rather than after they rust.
7 Common Problems and Their Fixes
- Heavy dross on the bottom edge. Raise gas pressure, then reduce feed rate slightly. Check that the nozzle orifice is clean and the right size.
- Rough or scalloped edge. Usually feed rate too high or focus too deep for the gauge. Also check for a zinc-coated nozzle affecting gas flow.
- Chalky white deposit beside the kerf. Condensed zinc oxide. Cosmetic; wipes off. Heavier deposits point to weak extraction.
- Spatter welded to the nozzle after the pierce. Use a staged pierce with lower initial gas pressure. Inspect the protective window; it takes the same hit. Our post on fiber laser cut quality problems covers pierce-related defects.
- Wide dark burn-back band along the edge. Too slow, too much power for the gauge, or oxygen where nitrogen or air should be used.
- Height sensing errors mid-sheet. Zinc oxide on the nozzle face. Clean or replace the nozzle and recalibrate the sensor.
- Operators reporting chills or flu symptoms after a galvanized run. Stop and check extraction immediately. This is metal fume fever, and it means fume is escaping the enclosure or filters are exhausted.
Frequently Asked Questions
Is it safe to laser cut galvanized steel?
Yes, on an enclosed machine with a properly functioning fume extraction system. The hazard is zinc oxide fume, and the enclosure plus the dust collector are what manage it. Cutting galvanized on a machine with weak or bypassed extraction is not safe.
Does galvanized steel cut slower than bare steel?
Slightly, in most shops. The zinc adds melt and vapor that the assist gas has to clear, so feed rates typically come down a modest amount from bare steel at the same gauge. Electrogalvanized cuts closest to bare steel speed; heavy hot-dip coatings cost the most.
Can I use oxygen on galvanized steel?
You can, but the edge will be rougher, with more dross and a wider burn-back band, because the oxygen reacts with the zinc as well as the steel. Nitrogen or air produces a cleaner result on sheet. Oxygen is mainly worth considering on thick hot-dip plate.
Will the cut edge rust?
The cut face is bare steel. Indoors, the surrounding zinc usually protects it for a long time through sacrificial action. Outdoors or in wet environments, plan on painting the edges, applying a zinc-rich touch-up, or galvanizing after fabrication.
Does cutting galvanized wear out consumables faster?
Nozzles and protective windows see more spatter and zinc oxide buildup than on bare steel, so inspect them more often. Dust collector filters load faster as well. Our laser machine spare parts guide covers what to keep on hand.
Cut Coated Steel With Confidence
Laser cutting galvanized steel is routine work once the gas, the parameters, and the extraction are set up for it, and the parts it produces are as good as anything you cut from bare sheet. Reger Laser sells, installs, services, and trains on Tanaka fiber lasers for fabrication shops nationwide, and material setup like this is part of every installation and training visit. See what our service covers or get in touch if you want help dialing in coated material on your machine.

