Reger Laser

Training & Safety

Operator training and laser safety for fiber laser cutting.

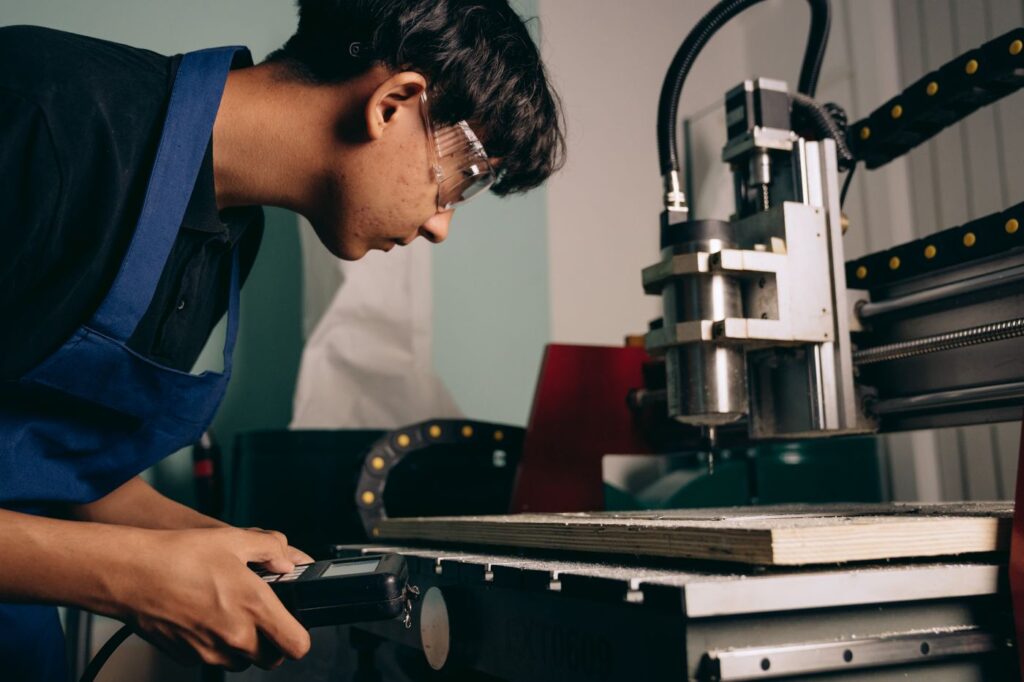
Machine operator wearing safety glasses while running equipment, the person who owns the laser shift start checklist
Maintenance & Service, Training & Safety

What Should a Laser Operator Check at the Start of Every Shift?

A good laser cutter daily checklist covers five areas before the first program runs: safety systems, the cutting head and optics, assist gas, cooling, and the table and motion system. Once an operator has done it a handful of times it becomes a short routine, and it catches most of the problems that otherwise show up halfway through a nest as dross, a burned protective window, a pierce that will not go through, or a head collision. The shops we see with the fewest emergency calls are not the ones with the newest machines. They are the ones where every operator checks the same things in the same order at the start of every shift. The checklist below is a starting point built from the service calls we get most often. Adjust it to your machine’s manual, post it at the control, and make it part of how every new operator is trained. Table of Contents Why a Laser Cutter Daily Checklist Matters Safety Systems Cutting Head and Optics Assist Gas Chiller and Cooling Tables, Slats, and Motion End of Shift Making the Checklist Stick Frequently Asked Questions Why a Laser Cutter Daily Checklist Matters Reger Laser services and supports fiber and CO2 cutting machines for fabrication shops across the country, and a lot of the repairs we do trace back to something that was visible at the start of the shift. A window with a spatter mark. A nozzle with a nick. A chiller running a few degrees warm. Gas pressure a little low because a bottle was near empty. Each of those is a two-minute fix before the first cut and a much bigger problem after a few hours of production. A daily checklist also makes a shop less dependent on one experienced operator. When the routine is written down, the second shift and the new hire check the same things the veteran does. That consistency is the whole point of the operator training we provide, and it is the foundation of any preventative maintenance program. Safety Systems Start with the things that protect people, because a machine that cuts perfectly with a bypassed interlock is not a machine anyone should run. Walk the machine and confirm guards, enclosure panels, and viewing windows are in place and undamaged. Test the emergency stops and confirm door and light curtain interlocks stop the machine. Confirm the fume extraction or dust collector is running and not alarming. Clear the area around the machine of scrap, tools, and anything that could trip someone or catch fire. Confirm a fire extinguisher is in its place and charged. OSHA’s guidance on machine guarding and its laser hazards overview are good references for why these checks matter. The laser beam in most cutting machines is infrared and invisible, so the enclosure and interlocks are what keep it where it belongs. Cutting Head and Optics The cutting head is where most daily problems start, and it is the area most worth a careful look. Protective window. Inspect it under good light for haze, pits, or burn marks, and replace it if you see any. Our guide to the laser protective window covers what to look for. Nozzle. Check the orifice for spatter, nicks, and roundness, and confirm it is seated tight. See our laser cutting nozzle guide for how damage shows up in the cut. Beam centering. Run a centering check if the machine or the nozzle has been changed or bumped. Height sensing. Calibrate the capacitive height sensor after a nozzle change, and confirm it responds. Focus. Confirm focus settings match the material in the first program. Assist Gas Assist gas problems look like cutting problems, so they are easy to misdiagnose. Checking supply before the first cut saves a lot of confusion later. Confirm there is enough oxygen, nitrogen, or air on hand for the shift’s jobs. Check that supply pressure at the regulator matches what the machine needs. Listen for leaks at fittings and hoses, and look for damaged lines. If the shop uses compressed air as an assist gas, drain the separators and confirm the dryer is working, because oil and water in the air end up on the optics. Our assist gas guide explains how each gas affects the cut and what purity and pressure problems look like on the part. Chiller and Cooling Confirm the chiller is running and holding its set temperature before the source is turned on. Check the coolant level and look for leaks under the chiller and along the lines. Confirm the condenser and filters are not clogged with dust. Note any chiller alarms, even ones that cleared on their own. A chiller that runs warm will not always stop the machine right away, but it shortens the life of the source and the optics. If the chiller is struggling, our post on why a laser chiller overheats walks through the usual causes. Tables, Slats, and Motion Look at the slats. Heavy slag buildup lifts sheets, causes tip-ups, and leads to collisions. Confirm the shuttle tables move freely and nothing is caught in the exchange path. Clear scrap from the bed and the conveyor or scrap bins. Home the machine and listen for new noises from the axes as it moves. Check the drive rails for debris that could reach bearings and racks. End of Shift The last five minutes of a shift set up the next one. Clean the head area, empty scrap bins, note anything unusual in a machine log, and report problems instead of leaving them for the next operator to discover. A shared log turns a vague complaint like “it has been cutting funny” into something a technician can actually diagnose. A good end-of-shift log does not need to be elaborate. Record the date, the operator, the materials cut, any alarms, any consumables changed, and anything that sounded, looked, or cut differently than usual. Over a few months that log becomes one of the most useful tools a technician has, because

Laser Cutting, Training & Safety

Essential Safety Tips for Operating Laser Cutting Machines

Laser cutters unleash an invisible beam powerful enough to slice through metal—yet that precision comes with hazards. A single misstep can cause severe injury, fires, or toxic fume exposure. Whether you’re scaling up to a multi‑shift operation or teaching a friend to use your desktop cutter, embedding safety into your workflow is non‑negotiable. Here’s how to build a culture of safety around your laser cutter. 1. Personal Protective Equipment (PPE) Essentials 2. Ventilation & Air Quality Appropriate fume extraction not only protects health but also prevents lens contamination. 3. Fire Prevention & Response Materials like wood or leather can smolder unexpectedly. Quick Tip: Label emergency stop buttons with glow‑in‑the‑dark tape for visibility. 4. Machine Inspection & Maintenance Regular checks uncover issues before they escalate. 5. Training & Standard Operating Procedures Building a Safety‑First CultureSafety isn’t a one‑and‑done. Host quarterly safety huddles, share lessons from incidents (yours or the industry’s), and reward employees who flag hazards. An empowered team is a safer team. Conclusion & ResourcesDownload our Laser Safety SOP Template to establish clear guidelines in your shop. Have questions? Reach out for a customized safety audit and keep your operation accident‑free.

Buying & Ownership, Laser Cutting, Training & Safety

An In-Depth Guide to Operating and Understanding Tanaka Laser Cutters

The Ultimate Guide to Tanaka Laser Cutters: Precision Meets Performance Tanaka laser cutters have become a household name in the world of precision cutting, renowned for their reliability, accuracy, and innovation. Whether you’re in manufacturing, engineering, or crafting, Tanaka laser cutters provide a seamless solution to meet your cutting needs. In this blog, we’ll explore the features, benefits, and applications of Tanaka laser cutters, helping you make an informed decision for your business. Why Choose Tanaka Laser Cutters? Tanaka laser cutters are known for their unparalleled precision. They utilize advanced technology to achieve micrometer-level accuracy and ensure flawless cuts every time. They offer wide material compatibility, handling everything from metals like steel and aluminum to non-metals like wood and acrylic with ease. These machines are designed for efficiency and speed, with optimized cutting paths and high-powered lasers that reduce production time without compromising quality. Additionally, Tanaka’s eco-friendly solutions align with sustainable manufacturing practices by minimizing material wastage and enhancing energy efficiency. Key benefits of choosing Tanaka laser cutters include: Key Features of Tanaka Laser Cutters Tanaka laser cutters are equipped with advanced features that make them stand out in the industry. They boast high-powered lasers capable of cutting through thick materials while maintaining fine detail. Their user-friendly interfaces, featuring intuitive control panels and software, ensure accessibility for both beginners and experienced professionals. Built with robust materials and cutting-edge engineering, these machines are durable and designed to last. Additionally, customizable settings allow users to tailor cutting parameters to suit specific projects and materials, ensuring versatility and precision. Key features include: Applications of Tanaka Laser Cutters These machines cater to a variety of industries, making them an essential tool for numerous applications. In the automotive industry, Tanaka laser cutters are used to cut components and do precision work. The aerospace sector benefits from its ability to cut lightweight yet durable materials with high precision. Signage and advertising professionals rely on Tanaka to create intricate designs and lettering. Artists and designers use these cutters to bring their visions to life through precise cuts and engravings, while jewelers craft delicate and detailed designs in precious metals with ease. Industries using Tanaka laser cutters include: Tips for Maximizing Efficiency with Tanaka Laser Cutters Regular maintenance is key to getting the most out of your Tanaka laser cutter. Cleaning lenses and mirrors and checking for software updates ensure consistent performance. Choosing materials Tanaka recommends will yield the best results, while proper training for your team helps unlock the machine’s full potential. Additionally, installing proper ventilation systems to handle fumes and debris generated during cutting will enhance safety and efficiency. Tips include: What Customers Are Saying Customers worldwide have praised Tanaka laser cutters for their transformative impact on various industries. Sarah L., a manufacturing engineer, noted, “Switching to a Tanaka laser cutter transformed our production line. The precision and speed are unmatched!” Marco R., a designer, shared, “As an artist, I rely on tools that deliver intricate details. Tanaka never disappoints.” James K., an operations manager, stated, “We’ve significantly reduced material waste since implementing Tanaka’s eco-friendly solutions.” Where to Buy Tanaka Laser Cutters If you’re ready to invest in a Tanaka laser cutter, there are several options to consider. Authorized dealers offer genuine products and warranties, ensuring peace of mind with your purchase. Reputable e-commerce platforms often feature Tanaka laser cutters with detailed specifications and customer reviews, making it easier to compare options. Additionally, visiting trade shows and expos allows you to see live demonstrations and consult with experts before making a decision. You can purchase from: Conclusion Tanaka laser cutters are a game-changer for anyone seeking precision, reliability, and efficiency in cutting and engraving. By investing in this advanced technology, you’re not just upgrading your tools – you’re empowering your business to achieve new heights. Discover the difference Tanaka laser cutters can make. Whether you’re crafting intricate designs or manufacturing industrial components, these machines are your trusted partner for success. Website design, hosting, and SEO done by datafanatics.com

Flat bed fiber laser cutting machine installed on a shop floor in a fabrication facility
Buying & Ownership, Maintenance & Service, Training & Safety

What Does a Fiber Laser Need to Be Installed? 7 Requirements to Check First

Fiber laser installation requirements come down to seven things: adequate and clean electrical service, dry compressed air, an assist gas supply, heat rejection through a properly sized chiller, a flat and solid floor, enough clearance for the machine plus material handling, and fume extraction with the right safety setup. Sort those out before the truck arrives and a machine goes from crate to first cut in a matter of days. Miss one and the machine sits. Most delayed installs we see are not machine problems. They are facility problems that nobody checked until the rigger was already on site. Below is what to verify, in the order it matters, with the questions to put to your electrician and your dealer well before the ship date. Table of Contents The Short Answer on What a Fiber Laser Needs A fiber laser is not a plug-in tool. It is a system that pulls significant three phase power, needs compressed air at a specified pressure and dryness, consumes assist gas, rejects a large amount of heat into a chiller, and has to sit dead flat and stay that way. It also needs room around it for sheets going in and parts coming out, and it produces fume that has to be captured. Every machine model publishes its own numbers for all of this. Do not work from a rule of thumb you read somewhere, and do not assume a new model matches the machine it replaced. Get the specification sheet for the exact machine and configuration you are buying, hand it to your electrician and your air and gas suppliers, and let them tell you what has to change. That is the whole job, and it is straightforward when it happens twelve weeks out instead of the week of delivery. What follows is the checklist to work through, and what tends to go wrong in each area. Requirement 1: Electrical Service and Power Quality This is the most common reason a fiber laser installation slips. A modern fiber laser plus its chiller and dust collector represents a serious load, and a lot of shops discover their existing service does not have the headroom once everything runs at once. Four things to confirm before ordering anything. First, the incoming service capacity, meaning whether there is enough amperage available at your panel with everything else in the shop running, not just on paper. Second, the voltage and phase the machine expects, since a mismatch means a transformer, and a transformer means lead time and floor space. Third, the disconnect and breaker sizing and where the disconnect has to be located relative to the machine. Fourth, grounding, which fiber lasers are particular about because the drives and the controller are sensitive to a poor ground. Power quality matters as much as capacity. Voltage sag when a large compressor kicks on, harmonic distortion from other drives in the building, and phase imbalance all cause faults that look like machine problems and are not. If your shop has a history of nuisance faults on other CNC equipment, get a power quality survey done before the laser lands rather than chasing it afterward. Work from the National Electrical Code and let a licensed electrician size the installation. One practical note: run the conduit and set the disconnect before the machine arrives. Riggers can place a machine in a morning. Waiting on an electrician afterward costs days. Requirement 2: Clean, Dry Compressed Air Compressed air runs the cutting head, the nozzle changer, the pneumatics, and on many machines it doubles as an assist gas for thinner material. It has to arrive at the pressure the machine specifies and it has to be dry. Dryness is where shops get hurt. Ordinary shop air carries water and compressor oil. Send that into a cutting head and you contaminate the protective window, which then absorbs energy, overheats, and fails, sometimes taking more expensive optics with it. The fix is a refrigerated or desiccant dryer sized for your actual air demand, plus coalescing filtration, plus a drain that works. Check the machine specification for the required dew point and filtration level and match it exactly. Volume is the second issue. A compressor that keeps up with hand tools may not keep up with a laser running air assist continuously. Size for the machine demand plus everything else in the shop running at the same time, and give it a receiver tank so short peaks do not drag the pressure down. Air quality problems show up as consumable cost first. If you are burning through protective windows and nozzles faster than expected, air is the first place to look, ahead of nozzle condition or cutting parameters. Requirement 3: Assist Gas Supply and Storage Assist gas is a facility decision, not just a consumable line item, because how you supply it changes what has to be built before the machine runs. Nitrogen for oxide free edges on stainless and aluminum, oxygen for thicker carbon steel, and air for lighter gauge each have different supply implications. High pressure cylinders are the simplest starting point and the most expensive way to run volume. Bulk liquid means a tank outside, a pad, a vaporizer, and a supplier agreement. On site nitrogen generation means a generator, more compressed air demand, and attention to purity, since nitrogen purity directly affects edge quality on stainless. Whichever route you choose, the piping run to the machine has to be sized for the flow the cutting head demands at pressure. Undersized line is a classic mistake: pressure reads fine at the manifold with the machine idle, then drops the moment cutting starts, and the edge quality goes with it. Regulators, manifolds, and cylinder or tank location all need to be settled before the install date, and outdoor bulk storage frequently involves a permit and a lead time measured in weeks. If you are still deciding, our breakdown of assist gas selection covers the tradeoffs between nitrogen, oxygen, and air by material and thickness.

Scroll to Top
0

No products in the cart.

No products in the cart.