
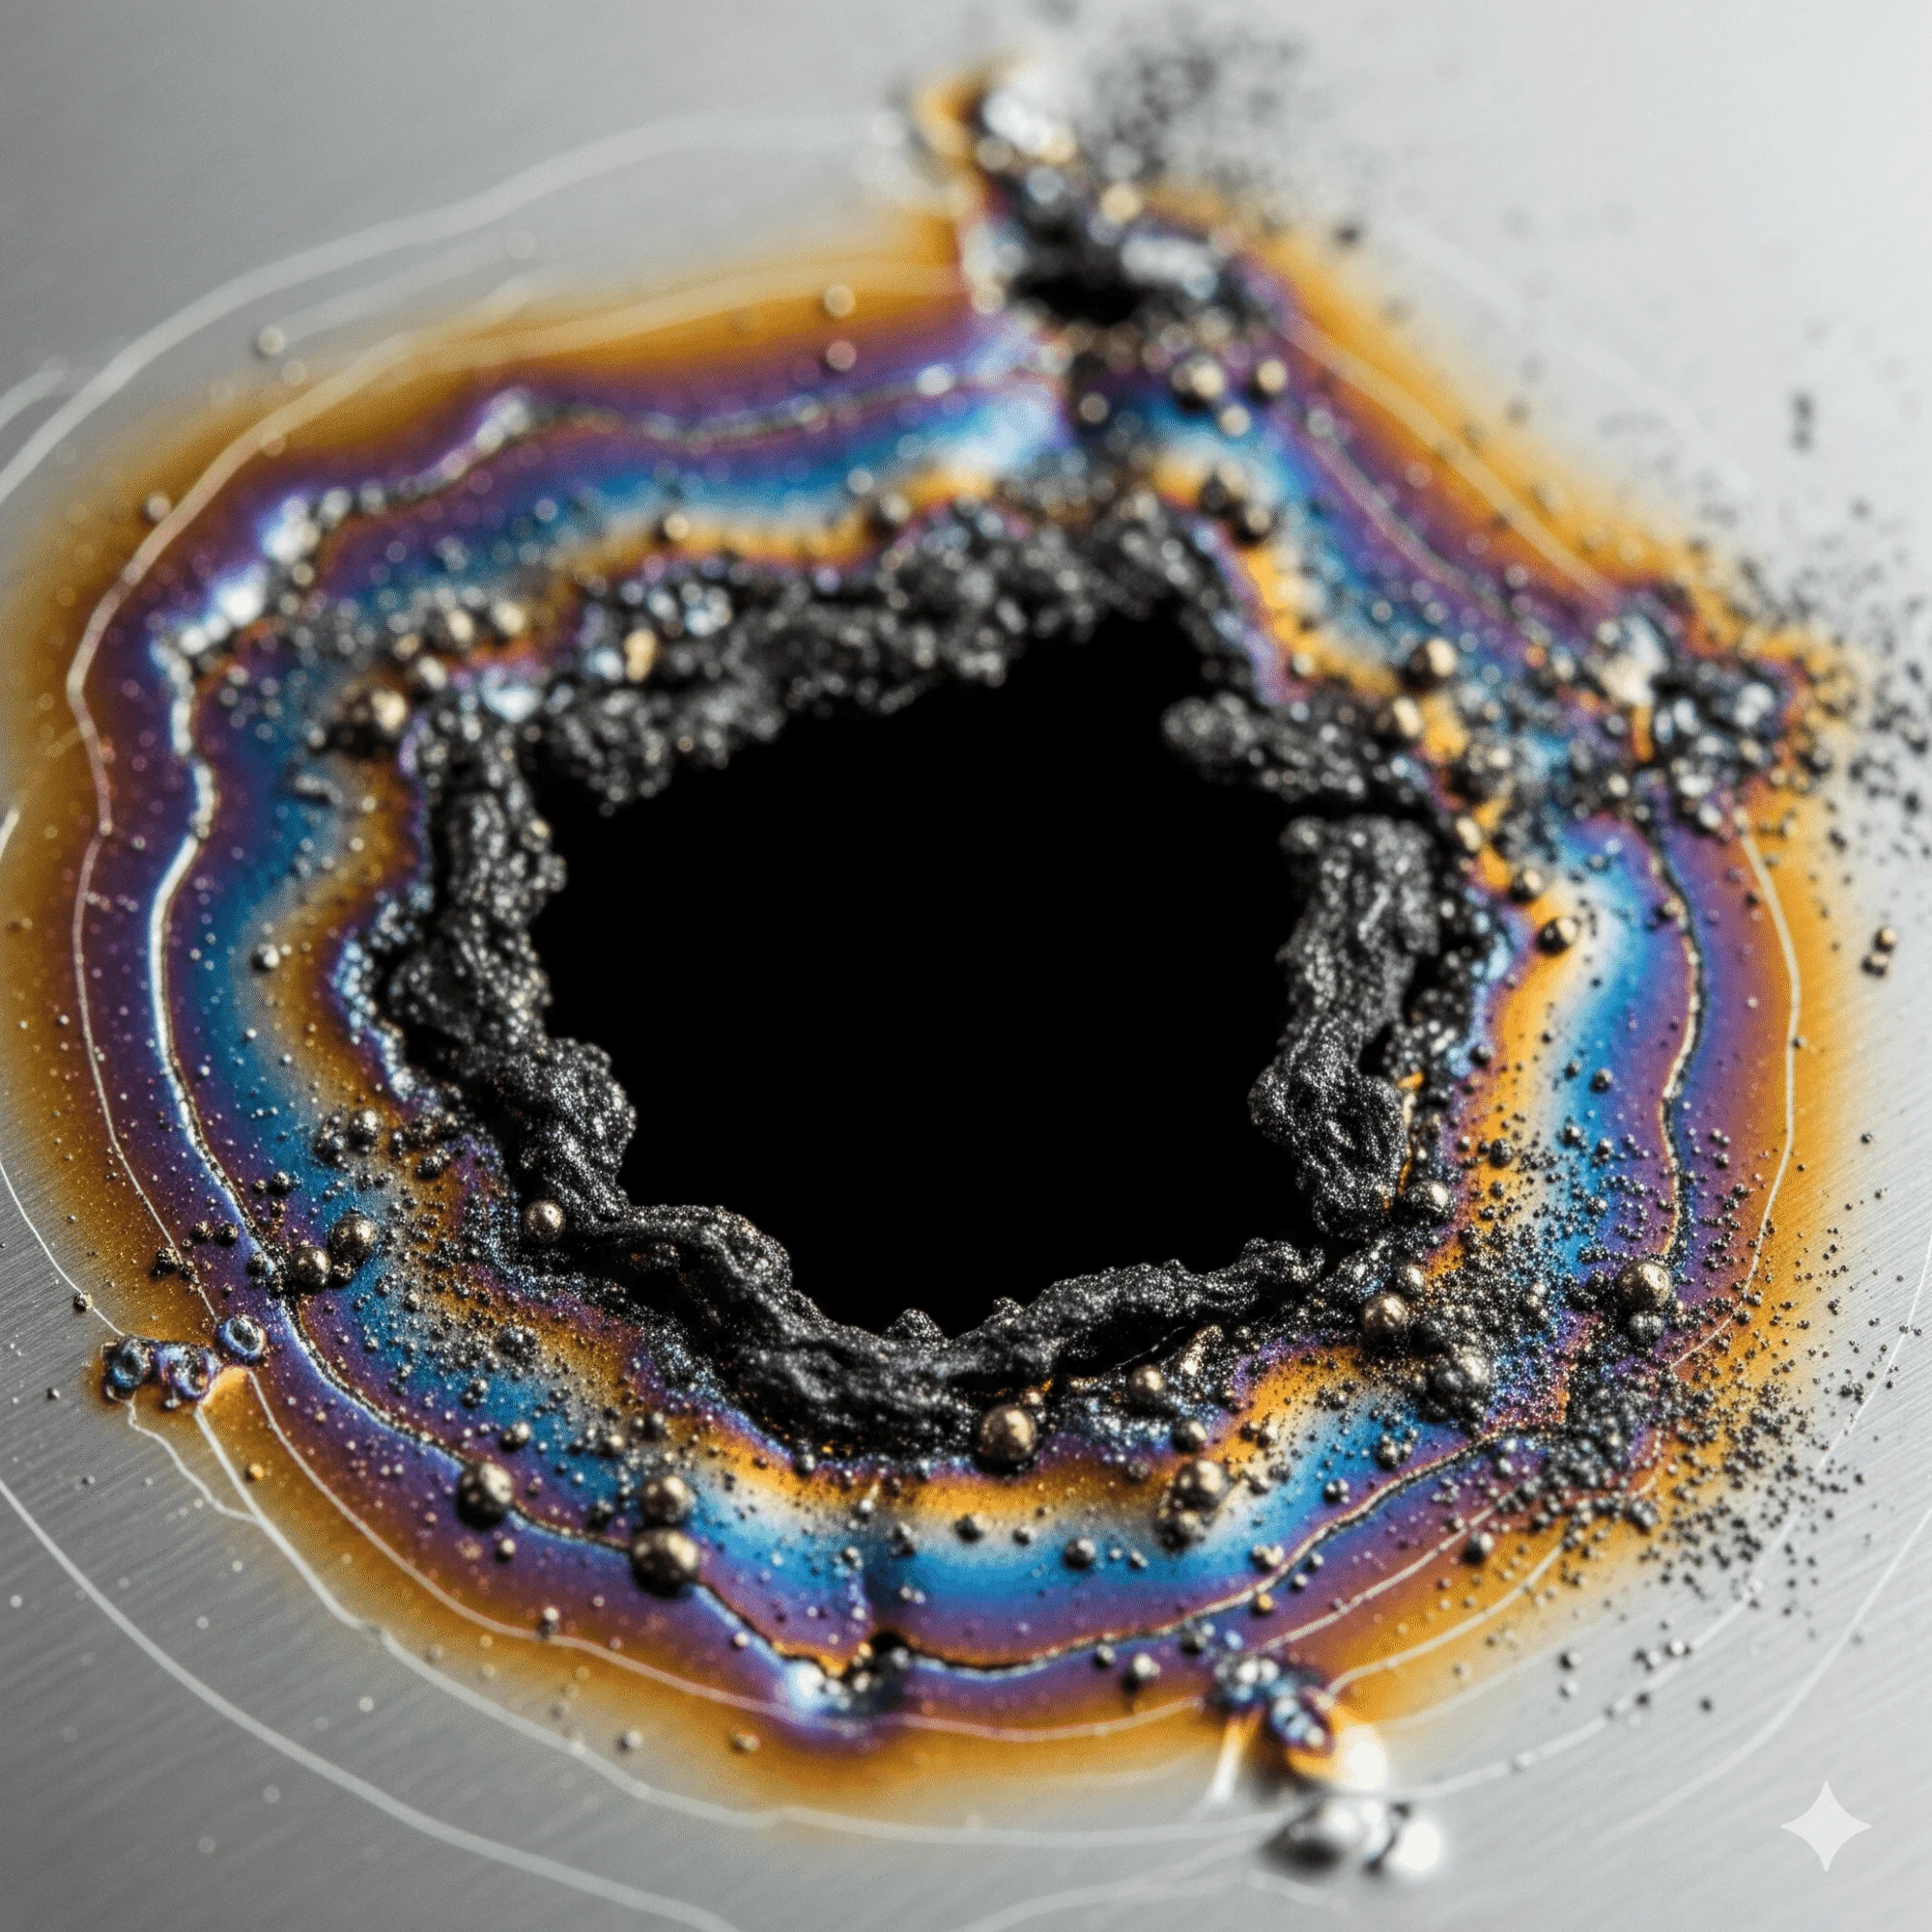
Fiber laser piercing problems show up as a pierce that never breaks through, a pierce that blows out into a crater, a shower of spatter that welds itself to the nozzle, or a first few millimeters of cut that look nothing like the rest of the part. Nine causes account for nearly all of them: a dirty protective window, an off-center or damaged nozzle, the wrong pierce focus, the wrong pierce time, gas pressure set for cutting instead of piercing, a contaminated plate surface, a standoff error, a pierce point placed too close to the contour, and a single-stage pierce on material that needs a ramped one.
The pierce is the hardest thing a laser does all day. It has to punch straight down through the full thickness with nowhere for the molten metal to go but back up at the head. Get it right and the rest of the cut usually takes care of itself. Get it wrong and you burn through protective windows, scrap parts, and lose cycle time on every hole. Here is how to diagnose piercing on a fiber laser, in the order that finds the cause fastest.
Table of Contents
- Fiber Laser Piercing Problems: The Short Answer
- What Happens During a Pierce
- Problem 1: A Dirty or Damaged Protective Window
- Problem 2: Nozzle Off-Center, Worn, or Wrong Size
- Problem 3: Pierce Focus Set for the Cut
- Problem 4: Pierce Time Too Short or Too Long
- Problem 5: Gas Pressure Set for Cutting
- Problem 6: Mill Scale, Rust, Oil, or Paint
- Problem 7: Standoff and Height Sensing Errors
- Problem 8: Pierce Point Too Close to the Contour
- Problem 9: Single-Stage Pierce on Thick Plate
- A 5-Minute Pierce Check Before Every Shift
- Frequently Asked Questions
Fiber Laser Piercing Problems: The Short Answer
Start at the head and work outward. Check the protective window, then the nozzle, then the pierce parameters, then the material, then the program. The first two are consumables that degrade every shift and cause the majority of sudden pierce failures on a machine that was cutting fine yesterday. Parameters cause problems when material or thickness changes. Material and program problems tend to be repeatable in one spot on one job.
Piercing is also where poor cut quality often begins, so if your parts have a bad lead-in, a crater at every hole, or dross near the start of each contour, fix the pierce before you touch cutting parameters. Our broader fiber laser troubleshooting guide covers what comes after.
What Happens During a Pierce
At the start of every contour the head stops, the beam fires straight down at a fixed point, and assist gas blows into the hole that forms. The metal melts from the top down, and because there is no kerf yet, the only exit for molten material is upward, past the nozzle. Once the beam breaks through the bottom, the gas can blow the melt down and out, the head starts moving, and the cut begins.
Everything that goes wrong in a pierce goes wrong in those few hundred milliseconds. Spatter thrown upward lands on the nozzle and the protective window. If the pierce runs too long, the hole widens into a crater and the gas dynamics change. If it runs too short, the head starts moving before breakthrough and the cut is lost. Modern machines manage this with ramped power, stepped gas, side air blow, and sensors that detect breakthrough, but they still depend on clean consumables and correct settings. The Fabricator’s piece on gaining an edge in fiber laser cutting covers how those pierce cycles have evolved.

Problem 1: A Dirty or Damaged Protective Window
The protective window sits below the focus lens and takes every bit of spatter the pierce throws up. A window with even light contamination absorbs beam energy, heats up, and scatters the beam, so less power reaches the plate and the focus shifts. Pierces get slower and dirtier, which throws more spatter, which dirties the window faster. It is a spiral, and it is the single most common reason a machine that pierced fine on Monday will not pierce on Thursday.
Fix: Inspect the window with a flashlight at an angle. Any haze, spots, or pitting means replace it, and on most fiber machines that takes a minute. Keep spares at the machine. If windows are dying fast, that is a symptom of a pierce problem further down this list, not a bad batch of windows.
Problem 2: Nozzle Off-Center, Worn, or Wrong Size
The nozzle has to be centered on the beam so the gas flows evenly around it. A nozzle that is off-center blows gas to one side of the pierce, the melt ejects unevenly, and the hole drifts. A nozzle with a spatter-clogged orifice or a worn tip changes the gas flow the same way. Using a larger nozzle than the pierce table calls for lowers the gas velocity at the hole; a smaller one can restrict flow enough that the melt never clears.
Fix: Run the nozzle centering routine after every nozzle change and any crash. Replace nozzles at the first sign of damage or buildup rather than cleaning them repeatedly, since a reamed-out orifice is no longer the size the table assumes. Match nozzle type and size to the material and thickness. Our laser cutting nozzle guide explains the types and when each applies.
Problem 3: Pierce Focus Set for the Cut
The focus position that cuts well is not always the focus position that pierces well. On thicker material, a pierce often wants the focus higher, at or above the surface, so the beam is wider where it first meets the plate and the melt has an easier path out. If the pierce uses the cutting focus, especially a deep negative focus set up for nitrogen cutting, the beam is tight and deep, the melt pool is narrow, and spatter rockets straight up the beam path.
Fix: Use the pierce focus from the manufacturer’s cutting tables, which is typically listed separately from the cut focus. When developing your own parameters, adjust pierce focus on its own rather than inheriting the cut value. Our post on fiber laser cutting parameters by material and thickness covers how the tables are organized.
Problem 4: Pierce Time Too Short or Too Long
On machines that run a programmed pierce time rather than sensing breakthrough, the time has to fit the material. Too short and the head moves off before the hole is through, and the beam plows into solid plate at cutting speed. The result is a lost cut, a spray of spatter, and often a nozzle strike. Too long and the beam keeps drilling a hole that is already open, widening it into a crater, heating the surrounding plate, and adding seconds to every pierce on the sheet.
Fix: Start from the table value and adjust in small steps while watching the pierce. The right time is the shortest one that reliably breaks through. Where the machine offers pierce detection, use it; it ends the pierce the moment the beam is through and removes the guesswork.
Problem 5: Gas Pressure Set for Cutting
Piercing and cutting want different gas pressures. Oxygen piercing at cutting pressure feeds an exothermic reaction with nowhere to go and blows the pierce out into a crater. Nitrogen piercing at too low a pressure fails to eject the melt, so the hole fills back in and never breaks through. Many controls run a lower oxygen pressure and a stepped nitrogen pressure during the pierce and switch to cutting pressure once through.
Fix: Confirm the pierce gas pressure is set separately from the cut pressure and matches the table for the material. Check that supply pressure at the machine is actually reaching the setpoint during the pierce; a regulator that sags under flow reads fine at rest and starves the pierce. Our guide to laser cutting assist gas covers oxygen, nitrogen, and air behavior in more depth.
Problem 6: Mill Scale, Rust, Oil, or Paint
The beam has to couple into the surface before anything else happens. Heavy mill scale, rust, oil, marking paint, or a protective film that was not meant to be cut through all change how the first millisecond goes. Scale flakes and pops, oil vaporizes and spatters, and paint burns. Any of them can produce an erratic pierce that behaves differently from one hole to the next on the same sheet, which is the signature of a material problem rather than a machine problem.
Fix: Buy pickled and oiled or descaled material for work where pierce quality matters, and wipe oily sheets before cutting. Remove protective films on the pierce side unless the film is specified as laser-cuttable. If a hot-rolled plate must be cut as-is, expect to use a gentler, longer pierce and place pierces away from the worst scale.
Problem 7: Standoff and Height Sensing Errors
The head uses capacitive sensing to hold a set distance from the plate. Spatter buildup on the nozzle, a warped or bowed sheet, or a plate lifted on a slat can fool the sensor, so the head sits too high or too low during the pierce. Too high and the gas loses velocity and focus moves; too low and the nozzle picks up spatter or strikes the melt.
Fix: Calibrate the height sensor on schedule and after every nozzle change. Keep the nozzle clean so the sensor reads the plate rather than the buildup. Flatten or re-support warped material, and program pierces away from unsupported edges where the sheet can spring.
Problem 8: Pierce Point Too Close to the Contour
A pierce placed right on the part edge or inside a tight feature puts the pierce crater, the heat, and the spatter on the finished part. The Fabricator’s guidance on designing parts for laser cutting makes the same point: heat and spatter from the pierce can damage the cut or lose it entirely when the pierce sits too close to the edge, and the best place for it is in the middle of a slug of material that will fall away.
Fix: Set the lead-in length in the nesting software so the pierce lands in scrap, and increase it on thick material where the pierce crater is larger. For small holes where there is no room for a lead-in, use the pierce-in-slug or a dedicated small-hole pierce strategy rather than piercing on the contour.
Problem 9: Single-Stage Pierce on Thick Plate
Thin sheet pierces in a fraction of a second at full power. Thick plate does not. Hitting half-inch or thicker plate with full power and full gas from the first millisecond throws a fountain of spatter, overheats the plate around the hole, and often blows out. The right approach ramps power up in steps, holds the gas low at first, and uses side air blow to push the spatter sideways instead of straight up. The result is a smaller hole, less spatter, and a longer life for the window and nozzle.
Fix: Use the multi-stage or ramped pierce settings your machine provides for thick plate, and use the table values as the starting point. If your machine offers a pierce detection sensor, pair it with the ramped pierce so the cycle ends the moment it breaks through.
A 5-Minute Pierce Check Before Every Shift
- Inspect the protective window and replace it if it shows any haze or spots.
- Inspect the nozzle for buildup or damage, replace if needed, and run the centering routine.
- Calibrate the height sensor.
- Confirm the pierce parameters loaded match the material on the table: focus, time, gas type, and gas pressure.
- Watch the first two pierces on the sheet and stop if either one spatters heavily or fails to break through.
Five minutes at the start of the shift catches nearly every consumable-driven pierce failure before it costs a sheet. It fits alongside the daily items in our fiber laser maintenance guide.
Frequently Asked Questions
Why does my fiber laser pierce fine on thin sheet but fail on plate?
Because thick plate needs a different pierce, not just a longer one. Focus, gas pressure, and power ramping all change with thickness, and a single-stage pierce that works on 14 gauge will struggle on half-inch. Use the plate pierce parameters from the tables and a ramped pierce cycle.
How often should protective windows be replaced?
As soon as they show contamination, which in a busy shop can be daily on thick plate work and weekly on thin sheet. A window is far cheaper than the lens behind it or the scrap a bad pierce produces. If you are replacing them constantly, address the pierce problem throwing the spatter.
Can a bad pierce damage the cutting head?
Yes. Spatter that gets past a damaged window reaches the focus lens, and a nozzle strike from a failed pierce can bend the head or damage the sensor. Both are expensive repairs that a clean window and correct parameters prevent.
Does pierce quality affect the rest of the cut?
Often. A crater at the pierce changes gas flow at the lead-in, and the heat from a long pierce can affect the first part of the contour. Many cut quality complaints trace back to the pierce, which is why we cover it before cutting parameters in our post on fiber laser cut quality problems.
Who can help dial in piercing on a Tanaka machine?
Reger Laser provides service, parts, and operator training for Tanaka fiber lasers nationwide, and pierce setup is part of every installation and training visit. Contact us with the material and thickness you are fighting and we will work through it with you.
Get the Pierce Right and the Cut Follows
Most fiber laser piercing problems come down to a consumable that needs changing or a parameter borrowed from the cut, and both are fixable in minutes once you know where to look. Reger Laser sells, installs, services, and trains on Tanaka laser cutting machines for fabrication shops nationwide. See what our service covers or get in touch if your pierces are costing you parts.