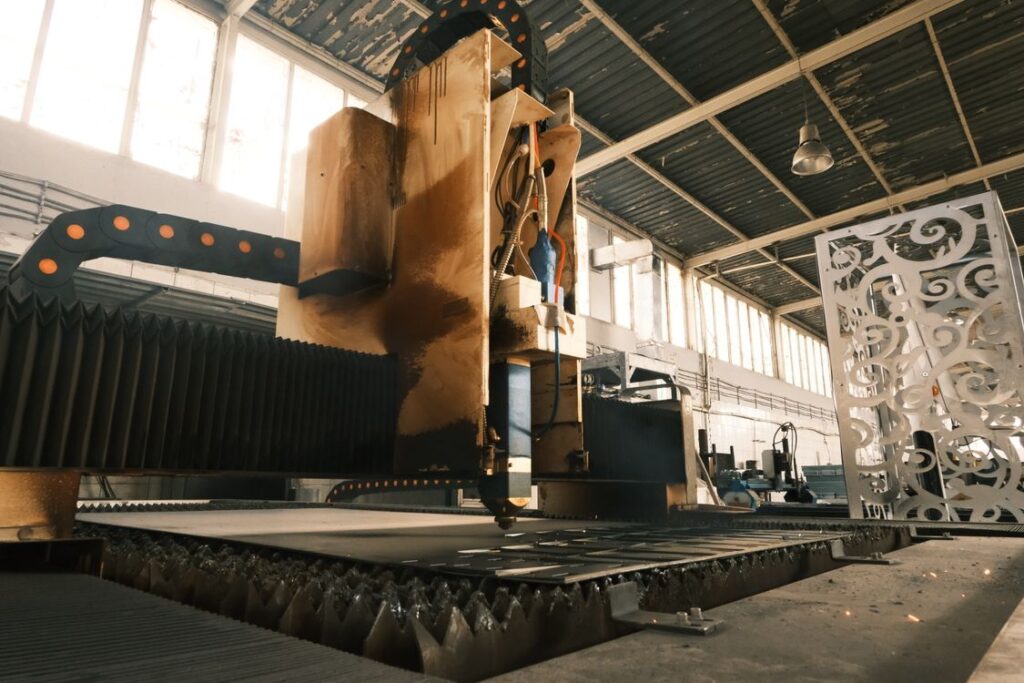
Fiber Laser Cutting Speed: What Controls It
Power, material thickness, assist gas, nozzle, and focus all set fiber laser cutting speed. Here is how each works and how to cut faster without ruining the edge.
Your blog category
Power, material thickness, assist gas, nozzle, and focus all set fiber laser cutting speed. Here is how each works and how to cut faster without ruining the edge.
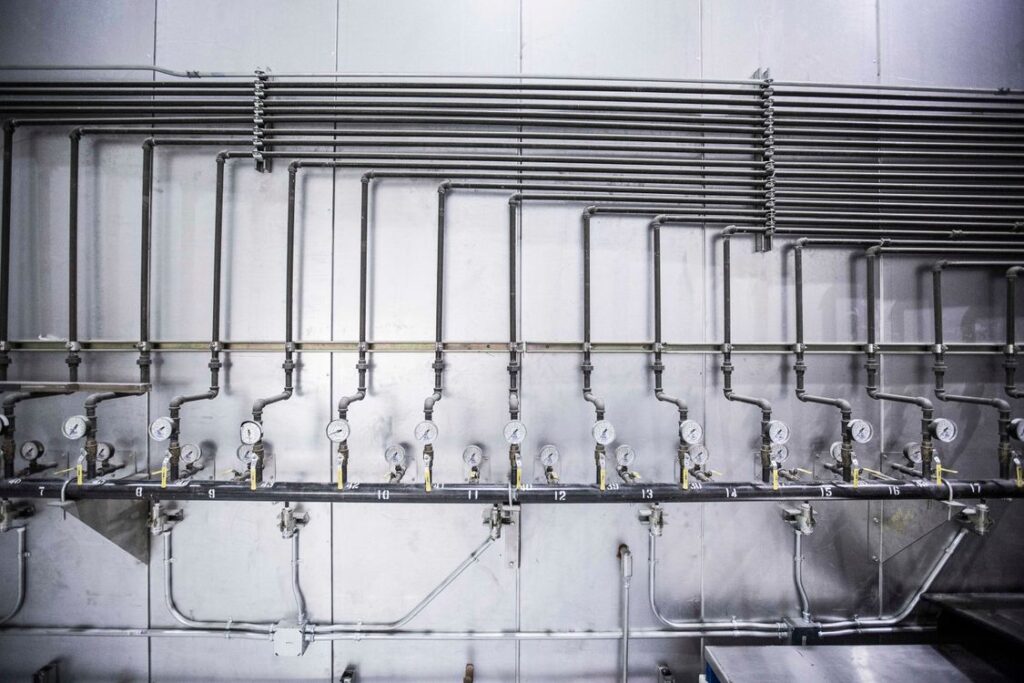
When to use oxygen, nitrogen, or shop air, why purity and pressure matter, and how the right laser cutting assist gas controls both edge quality and cost.
How Tanaka fiber lasers work, why they beat CO2 on cost and uptime, the full lineup, materials, service, and how to choose new vs used.
The four variables behind almost every edge defect, how to fix dross, striations, and burr, and how ISO 9013 actually measures laser cut edge quality.
Kerf in laser cutting is the width of material the beam removes. What changes it, why it moves parts out of spec, and how shops compensate.

Water quality, coolant changes, condenser cleaning, and reading chiller faults. The laser chiller maintenance routine that keeps your source out of an over-temp fault.

Power, speed, focus, and gas explained, how the settings change by material and thickness, and how to build a parameter library.
Why cooling matters, matching capacity and stability to the machine, flow and coolant, ambient conditions, and the common sizing mistakes.
How a fiber source is built, how long it lasts, how it ages, what extends or shortens its life, and why it outlives CO2.

What calibration covers, beam centering, focus, height sensor and axis checks, when to do each, and operator tasks vs service work.